

 Current location:
Why Precision Tooling Matters in Modern Manufacturing
2026-08-18There is a moment in every manufacturing operation when the difference between a good tool and a mediocre one becomes impossible to ignore. It shows up in the part rejection rate that jumps after a tooling change, or in the customer complaint about surface finish on a batch that was supposed to be routine. Precision tooling is one of those factors that gets taken for granted until it is gone. For buyers and engineers making tooling decisions, understanding what actually drives precision—and where imprecision costs money—is worth the effort because the returns are real and measurable.
What Precision Actually Means in Industrial Tooling
The word precision gets used loosely in manufacturing conversations, but when it comes to tooling, the technical definition matters. Precision refers to the deviation between the nominal dimensions specified in a design and the actual dimensions produced in the tool. A die bore specified as 2.000 millimeters that actually measures 1.998 millimeters has a deviation of 0.002 millimeters. Whether that is acceptable depends entirely on what the downstream process requires.
In practice, precision means different things in different contexts. For a wire drawing die used in electrical conductor production, a deviation of 0.005 millimeters on a 1.0 millimeter bore might be perfectly acceptable. For a medical guidewire die producing 0.08 millimeter wire, the same 0.005 millimeter deviation represents over 6 percent of the total diameter—completely unacceptable. Understanding where your application falls on this spectrum is the first step in specifying tooling that is precise enough without paying for precision you do not need.
Manufacturers who source precision tooling without understanding their own tolerance requirements tend to either over-specify (paying premium prices for precision that their process does not use) or under-specify (accepting tooling that causes downstream quality problems). Neither outcome serves the business well.
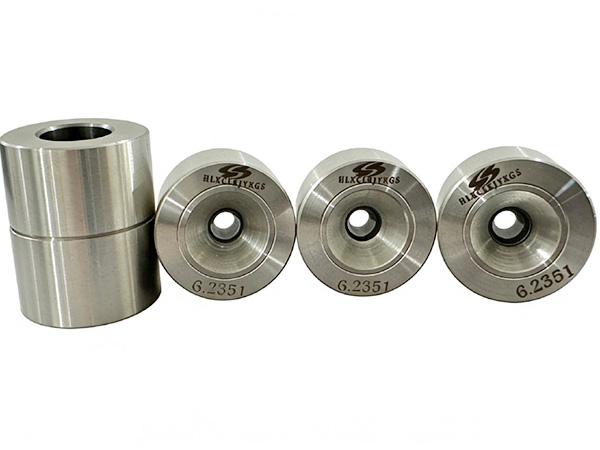
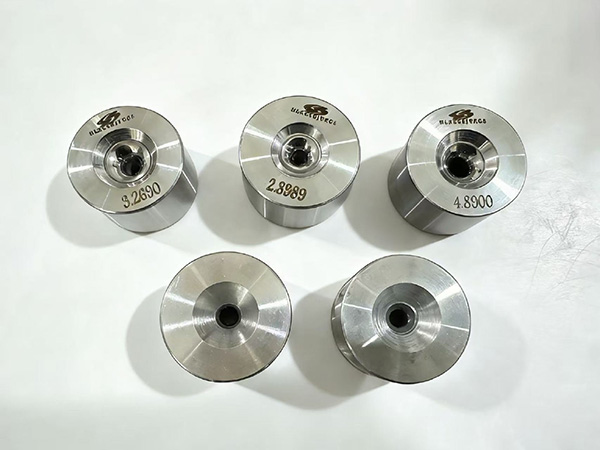
Where Imprecision Costs Money
The costs of imprecise tooling are rarely visible on the tooling invoice. They show up downstream, buried in scrap reports, rework logs, and customer complaints that trace back to decisions made weeks or months earlier when the tooling order was placed.
Scrap is the most obvious cost. When a tooling component produces parts outside specification, those parts either get reworked (adding labor cost) or scrapped (adding material cost). In high-volume operations, even a one percent increase in scrap rate from tooling variation can represent hundreds of thousands of dollars per year in lost material and labor. A supplier who quotes a slightly lower price on tooling but delivers inconsistent precision will cost more than a premium supplier over the life of the tooling.
Downtime from tooling-related quality events is another hidden cost. When a die begins producing out-of-specification parts, there is a lag between the onset of the problem and its detection by quality control. During that lag, every part produced is potentially scrap or rework. In operations running 24/7, even a few hours of undetected imprecision can generate a significant scrap pile. Preventive die replacement schedules, based on measured wear rather than calendar time, reduce this lag and the associated scrap costs.
Customer quality incidents carry costs that are even harder to quantify but no less real. A customer who receives a shipment of parts with surface defects or dimensional variation will not just return the bad parts—they will audit the supplier's quality system, potentially impose incoming inspection requirements, and may quietly shift future volume to a competitor. The cost of one quality incident can exceed the tooling budget for an entire year.
The Relationship Between Tool Tolerance and Product Tolerance
Every manufacturing process has a tolerance stack-up—the accumulated effect of variation from each step in the process. Tooling precision is typically the first element in this stack, and it sets the ceiling for what the downstream process can achieve. No amount of process optimization can produce parts more precisely than the tooling that forms them allows.
A useful rule of thumb is that tooling precision should be at least four times better than the product tolerance it must produce. A die that must produce wire within ±0.01 millimeters should itself be held to ±0.0025 millimeters or tighter. This ratio provides a margin that prevents tooling variation from consuming the entire product tolerance budget, leaving room for process variation from other sources.
Manufacturers who apply this ratio consistently find that their process capability indices improve, their scrap rates drop, and their customer quality metrics become more stable. It is a straightforward engineering principle, but it requires the discipline to specify it clearly when ordering tooling and to verify it when the tooling arrives.
Surface Finish as a Precision Driver
Precision in tooling is not only about dimensions. Surface finish on tooling components is equally consequential for many applications, particularly in forming, drawing, and extrusion operations where the tool surface contacts the product directly.
For wire drawing dies, the bore surface finish directly determines the wire surface that emerges from the drawing process. A die bore with Ra surface roughness of 0.05 micrometers will produce wire with approximately the same roughness value—potentially flawless for magnet wire applications. A die bore at Ra 0.20 micrometers will produce wire with visible die lines and surface variation that fails inspection for most electrical applications.
The same principle applies across precision tooling types. Mated surfaces in forming dies, cavity surfaces in injection molds, and bearing surfaces in progressive dies all transfer their surface texture to the products they make. When surface quality matters for the product, it must matter for the tooling that produces it.
Supplier Qualification: Verifying Precision Before Purchase
Buying precision tooling without verifying the supplier's actual manufacturing precision is one of the most common procurement mistakes in manufacturing. The inspection report that comes with a die tells the buyer what that specific die measures, but it does not reveal the process capability that produced it or whether the next batch will measure the same way.
A more meaningful qualification approach involves requesting process capability data from the supplier. Ask for the Cpk values on the critical dimensions of the tooling types you plan to purchase. A Cpk above 1.33 indicates a capable process; above 1.67 indicates excellent control. A supplier who cannot or will not provide this data is essentially asking the buyer to accept their tooling quality on faith.
Sample lot trials are another valuable qualification tool. Order a small lot of production samples and measure them thoroughly. Track the dimensional variation, surface finish consistency, and any other quality attributes that matter for your application. A supplier's first article inspection data tells you what one die can do; a sample lot trial tells you what their production process consistently does.
Precision Tooling as a Competitive Advantage
Manufacturers who treat precision tooling as a strategic investment rather than a commodity purchase consistently outperform those who do not. The mechanism is straightforward: better tooling produces better parts, better parts generate fewer quality incidents, fewer quality incidents preserve customer relationships, and preserved customer relationships translate into stable and growing revenue.
This competitive advantage compounds over time. A supplier who consistently delivers parts with tighter dimensional control and better surface finish builds a reputation that commands premium pricing and preferential treatment from customers who value quality over lowest price. A supplier who chases tooling cost reductions eventually ends up with a quality reputation that limits their access to the most demanding customers.
The buyers and engineers who make tooling decisions have more influence over this outcome than they often realize. The choice of tooling supplier, the specification of precision requirements, and the verification of incoming tooling quality all shape the quality of what the factory produces. Those decisions deserve the same analytical rigor applied to other manufacturing investments.
Frequently Asked Questions
Q1: How do I determine the right precision level for my tooling?
Start with your product tolerance requirements. Apply a 4:1 precision ratio: your tooling should be held to tolerances at least four times tighter than the product tolerance it must produce. This provides margin for process variation from other sources and ensures that tooling variation does not consume your full tolerance budget.
Q2: Is the most precise tooling always the best choice?
No. Precision has a cost, and that cost should be proportionate to the benefit. If your product tolerance is ±0.05 millimeters, specifying tooling to ±0.001 millimeters adds cost without adding value. Match your tooling precision to your actual product requirements rather than specifying the tightest available tolerance by default.
Q3: What inspection data should I require from a precision tooling supplier?
Request dimensional measurement reports for every critical dimension, surface roughness measurements for all functional surfaces, and geometric tolerance verification (concentricity, perpendicularity, flatness as applicable). All measurements should be traceable to calibrated instruments with current calibration certificates.
Q4: How can I verify that a supplier maintains precision consistently over time?
Request statistical process control data showing dimensional variation over recent production runs. Ask for Cpk values on the critical parameters. Conduct periodic incoming inspections on sample dies from production batches to verify that the supplier's stated quality is being maintained in practice.
Q5: What is the total cost impact of imprecise tooling beyond the purchase price?
Imprecise tooling generates costs in scrap, rework labor, downtime from quality events, and customer quality incidents. In high-volume operations, these hidden costs typically exceed the tooling purchase price by 3 to 10 times over the tooling's service life. The lowest-price tooling is rarely the lowest-total-cost tooling.
Conclusion
Precision tooling matters because it sets the ceiling for what a manufacturing operation can produce. Imprecise tooling generates costs that hide in scrap reports, rework logs, and quality incidents—costs that almost always exceed any savings from buying cheaper tooling. Specifying the right level of precision for the application, verifying supplier capability before purchase, and monitoring incoming quality systematically transforms tooling from a commodity purchase into a strategic investment that supports product quality, customer relationships, and competitive position.
References
Montgomery, D. C., & Runger, G. C. (2023). Applied Statistics and Probability for Engineers. John Wiley & Sons.
Kalpakjian, S., & Schmid, S. R. (2022). Manufacturing Engineering and Technology. Pearson.
ASTM International. (2023). Standard Practice for Inspection and Verification of Industrial Dies and Molds (ASTM E2864-23). West Conshohocken, PA.
ISO Technical Committee TC 213. (2023). Geometrical Product Specifications and Verification (ISO 1101:2023). Geneva: ISO.
Schrock, J. R. (2022). The Economics of Precision in Industrial Manufacturing. Precision Engineering, 69, 142-156.